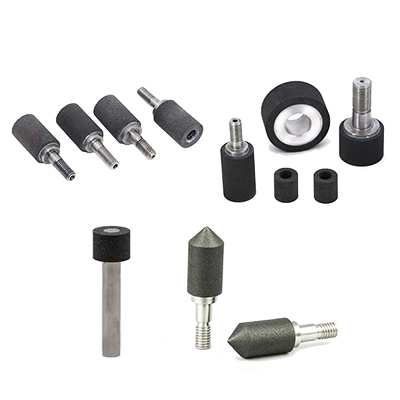
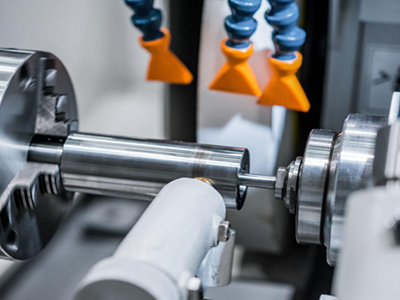
Vitrified CBN Internal Wheel for Bearing Races & Fuel Injector Bore Grinding
Write your message here and send it to us
Related Products
-
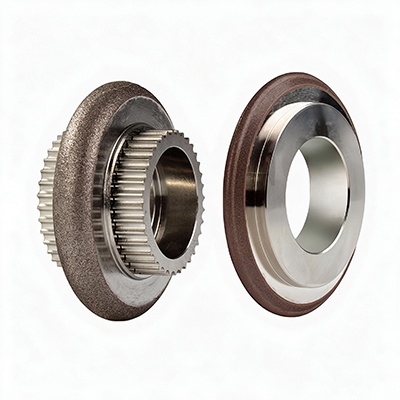
Electroplated CBN Form Wheel for Precision Aerospace Gear & Spline Grinding
-
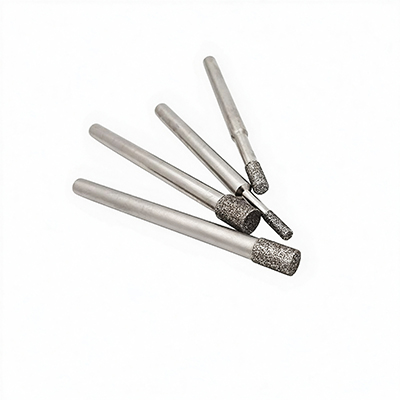
Electroplated CBN Grinding Pins for Precision Internal Grinding
-
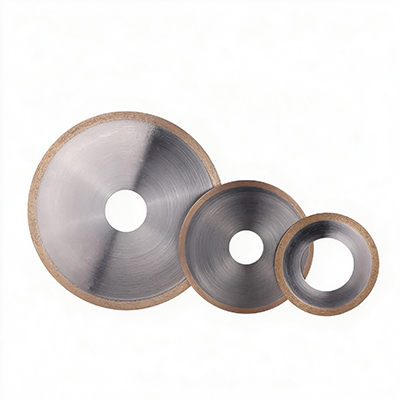
Sintered Metal Bond CBN Cut-Off Wheel for Hardened Steel Rods & Tubes
-
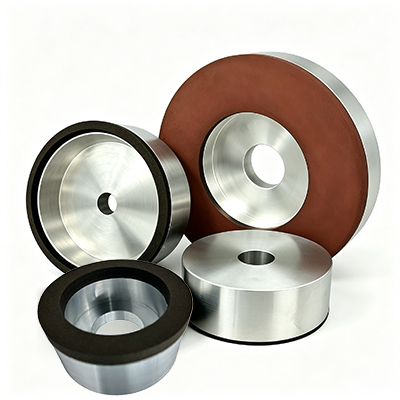
Resin Bond CBN Double Disc Wheel for Parallel Surface Grinding
-
Resin Bond CBN Centerless Wheel for High-Precision Steel Pins & Shafts
-
Resin Bond CBN Profile Wheel for Hardened Gear & Spline Grinding
-
Resin Bond CBN Wheel for HSS End Mill & Drill Fluting / Sharpening
-
Vitrified CBN Internal Wheel for Bearing Races & Fuel Injector Bore Grinding
-
Vitrified CBN Wheel for Automotive Crankshaft & Camshaft High-Speed Grinding